Reclaimed Asphalt Pavement (RAP) technology is transforming road construction from a supplementary material into a core circular solution by combining specialized plant equipment, precise process control, and robust material management to produce high-performance asphalt with reduced emissions and costs.
- RAP integration requires specialized technology: Hot recycling systems heat reclaimed material indirectly and blend it precisely with virgin materials, reducing binder ageing and maintaining performance standards.
- Material variability demands strict controls: Dedicated storage, pre-treatment processes, and defined protocols minimize differences in aggregate grading, binder ageing, and moisture content across RAP sources.
- Quality assurance is non-negotiable: Regular laboratory testing of binder content, ageing levels, and aggregate characteristics ensures consistent, repeatable mix designs and stable production.
- Proven large-scale deployment: A Lintec CSM4000HRC plant in China produced over 2 million tonnes of RAP asphalt, while Mexican installations successfully integrate up to 15% RAP in high-output applications.
- RAP requires system-level engineering: Success depends on integrating recycling into plant design, control systems, and operating processes rather than treating it as a simple add-on.
As sustainability, cost efficiency and resource security rise to the top of infrastructure agendas worldwide, Reclaimed Asphalt Pavement (RAP) is moving from a supplementary option to a core component of modern road construction. Governments, road authorities and contractors are increasingly recognizing RAP as a practical pathway to circularity, reducing reliance on virgin materials while lowering emissions and production costs.
While the environmental and economic case for RAP is clear, its successful implementation depends on far more than simply reintroducing reclaimed material into the asphalt mix. Achieving consistent quality, durability and performance requires the right plant technology, robust process control, and a disciplined approach to material management throughout the production and paving process.

RAP Integration
RAP integration is a technology challenge as much as a material one. Asphalt plants must be specifically equipped to introduce recycled material safely and efficiently, with the ability to control temperatures, material flow, and mixing conditions accurately. The selection of recycling technology, whether cold recycling or hot recycling, depends on project requirements, desired RAP percentages, and production capacity.
In practice, hot recycling systems are often preferred where higher RAP use and consistent output are required. These systems allow reclaimed material to be heated indirectly and blended more precisely with virgin aggregates and binder, reducing the risk of premature binder aging and maintaining asphalt performance.
Material handling is equally critical as RAP is inherently variable, with differences in aggregate grading, binder ageing and moisture content depending on its source. Dedicated storage areas, pre-treatment processes and clearly defined material management protocols are essential to minimize variability and ensure stable production. Without these controls, higher RAP percentages can compromise both quality and consistency.
Quality Control
Laboratory testing and quality assurance are essential for a successful RAP application. Regular analysis of RAP materials allows producers to understand binder content, aging levels and aggregate characteristics, forming the basis for accurate and repeatable mix designs.
During production, additional monitoring of temperatures, mixing times and emissions is required, particularly as RAP content increases. When these parameters are carefully managed, RAP asphalt can be produced to the same performance standards as conventional mixtures.
On site, the transition to RAP does not require fundamental changes to paving or compaction practices. When produced correctly, RAP mixtures can be laid, compacted, and assessed using the same methods applied to virgin asphalt, helping contractors adopt RAP without disrupting established workflows.

RAP Technology Experience
Rather than adopting a one-size-fits-all approach, RAP integration through configurable recycling systems can be adapted to specific project requirements. This includes adjusting RAP content, production capacity, and plant configuration, as well as optimizing heating, dosing, and mixing parameters to suit material characteristics and local conditions. By combining modular system design with precise process control, operators can manage variability in reclaimed materials while maintaining consistent mix quality and production stability across a wide range of applications.
One example is in Anhui Province, China, where hot recycling systems have been deployed extensively. In this region, a Lintec CSM4000HRC Asphalt Mixing Plant has produced more than two million tons of RAP asphalt, demonstrating that high-volume recycling can be achieved reliably over extended periods when supported by appropriate technology and process control.
In Latin America, RAP adoption is accelerating as infrastructure investment expands alongside sustainability expectations. Mexico will see supported elements of the federal government’s National Road Infrastructure Program, which includes large-scale road rehabilitation and new construction projects.
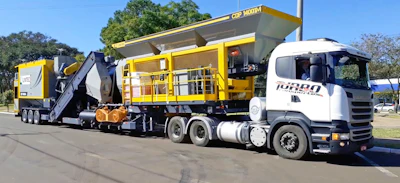
A key installation is the Lintec CDP14000M Asphalt Mixing Plant, designed for high output, mobility and rapid installation. The plant is capable of integrating up to 15% RAP while maintaining stable production and consistent mix quality, helping reduce raw material consumption and environmental impact without compromising performance on major road projects.
The key to RAP success lies in treating recycling as a system-level capability rather than a simple add-on. It is not just about adding recycled material into the mix. To achieve consistent quality and long-term performance, recycling must be engineered into the plant design, the control system and the operating process. When the right technologies and controls are in place, RAP can deliver significant environmental and economic benefits without compromising asphalt performance.
RAP's Role in the Future of Road Construction
As material costs continue to rise and sustainability requirements tighten, RAP is set to become an increasingly standard feature of asphalt production instead of a niche solution. Road authorities are embedding recycled content into specifications, while contractors are seeking proven technologies that allow them to meet these requirements consistently and at scale.
Combining recycling technologies with automation, modular plant design and process intelligence helps producers and contractors integrate RAP responsibly while maintaining the performance standards expected of modern road infrastructure.
By doing this, RAP becomes more than a sustainability initiative, delivering strategic capabilities that support circular construction, improving resource resilience and shaping the future of road building worldwide.